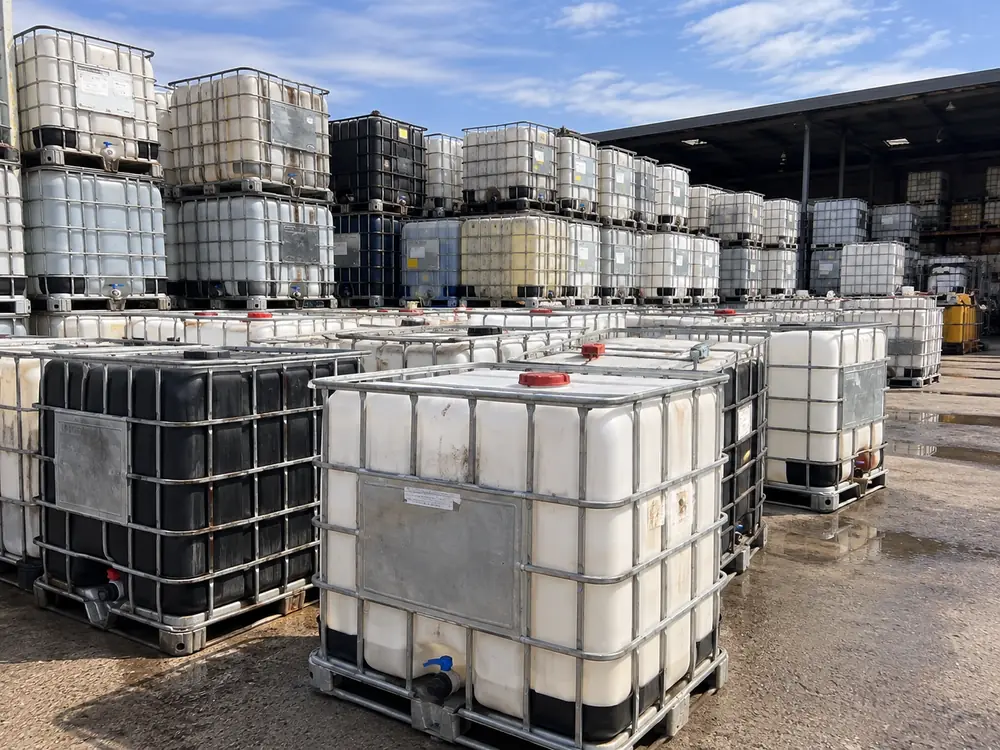
Totes for chemical & industrial use
The sector that buys the most Grade B containers and supplies the most empties. Here the decisions that matter are elastomer compatibility, density and marking status — not bottle clarity.
Quote industrial stock or a buy-back
Name the chemistry and the concentration. We will specify the valve, the seal and the grade in writing.
Tell us what you have.
We will tell you what it is worth.
Buying, selling, washing, hauling or recycling — one form covers all of it. Replies come from a specialist in York, PA, by email, inside one business day.
Prefer plain email? Write to info@ibctotesreco.com — include your ZIP, quantity and what the totes last held.
Industrial buyers should default to Grade B reconditioned and spend the saving on correct elastomers and the right valve. Switch to stainless for aromatic or chlorinated solvents, fuels, hot fill above 140°F, strong oxidisers and anything that needs validated cleaning. Check the marking status before buying if the container will carry a regulated material.
Three decisions, in priority order
1. Material of construction
Does your chemistry belong in polyethylene at all? HDPE handles acids, alkalis, salts, glycols, surfactants and most water-based formulations indefinitely. It does not handle aromatics, chlorinated solvents, ketones, fuels or sustained heat. Getting this wrong produces a slow failure — wall softening, permeation, odour, stress cracking — rather than an obvious one, which is why it goes unnoticed until it does not.
2. Elastomers
The gasket and valve seat are the parts that fail first and the parts nobody specifies. EPDM is right for water-based chemistry, dilute acids and alkalis, glycols and surfactants. Viton is right for aromatics, fuels, oils, fats and higher temperatures. PTFE handles nearly everything but demands a better sealing face. The compatibility table.
3. Marking and periodic test status
If the container will carry a DOT-regulated liquid, the marking has to be valid, the design type authorised for your material and packing group, and the periodic inspection and leak test current under 49 CFR 180.352. A container with a destroyed plate is a perfectly good industrial vessel for non-regulated service and is not an authorised packaging. We state which on every quote.
Density: the quiet one
Industrial chemistry is dense. A 275-gallon tote of 50% caustic soda is about 3,500 lb; 93% sulphuric acid is about 4,200 lb. Both exceed a great many rack beam levels, pallet jacks and lift gates that handle a water-filled tote without complaint. Run the numbers on the weights page before you order the format, not after.
Your empties are worth money
Blending plants are structurally net generators of empty containers: bulk liquid in, smaller packages out. Most plants we deal with were paying to have them removed before we quoted. Standing weekly or monthly collections, written offers, weight tickets and prior-contents records — how the buy-back works.
Industrial products in IBC service
Container material, seal and the thing to watch — per chemistry.
| Chemistry | SG | 275 gal filled | Container | Seal | Watch for |
|---|---|---|---|---|---|
| Sodium hydroxide 50% | 1.52 | 3,497 lb | HDPE | EPDM | Weight; crystallises when cold |
| Sulphuric acid 93% | 1.83 | 4,182 lb | HDPE (dedicated) | PTFE | Weight; heat on dilution |
| Hydrochloric acid 31% | 1.16 | 2,702 lb | HDPE | PTFE | Fume attack on cage |
| Sodium hypochlorite 12% | 1.21 | 2,812 lb | HDPE, UV-shielded | EPDM | Degasses; vent the lid |
| Hydrogen peroxide 35% | 1.13 | 2,635 lb | HDPE, dedicated | PTFE | Vent; no contaminants |
| Surfactant concentrate | 1.05 | 2,457 lb | HDPE | EPDM | Foaming on transfer |
| Propylene glycol coolant | 1.04 | 2,435 lb | HDPE | EPDM | Nothing — ideal duty |
| Calcium chloride brine | 1.38 | 3,187 lb | HDPE | Viton | Chloride attack on cage |
| Magnesium chloride de-icer | 1.32 | 3,054 lb | HDPE | Viton | Chloride; weight |
| Plating chemistry (nickel) | 1.25 | 2,901 lb | HDPE, dedicated | Viton | Never re-use for anything |
| Mineral oil / cutting fluid | 0.88 | 2,083 lb | HDPE | Viton | Permeation; odour |
| Mineral spirits / aromatics | 0.79 | 1,880 lb | Stainless | PTFE | Crazes HDPE |
| Acetone / ketones | 0.79 | 1,880 lb | Stainless | PTFE | Softens HDPE |
| Adhesive / resin emulsion | 1.08 | 2,523 lb | HDPE | EPDM | Ghosts permanently |
| Latex paint | 1.30 | 3,010 lb | HDPE | EPDM | Needs caustic CIP after |
Guidance for ambient service at stated concentration. Always verify against your product's safety data sheet and the container manufacturer's chemical resistance data; send us the product name and we will check it with you.
Chemical & industrial FAQ
Which grade should a chemical blender buy?
Grade B reconditioned, almost always. It is a washed, leak-tested, re-valved and re-marked container at roughly a quarter to a third of new-unit cost, and for industrial chemistry the staining that keeps it out of Grade A is cosmetically irrelevant. Spend the money you save on specifying the right elastomer instead — that decision matters far more than bottle clarity.
Can I ship a regulated liquid in a reconditioned tote?
Yes, if the container carries a valid current UN marking, has a passing periodic inspection and leak test on record, and the design type is authorised for your material and packing group. Selecting an authorised packaging is the shipper's legal duty, not the container supplier's. Our plain-English walkthrough of those obligations is on the hazmat shipping page.
What chemistries will destroy a poly tote?
Aromatic and chlorinated solvents swell and stress-crack HDPE. Ketones soften it. Fuels and oils permeate and permanently odourise it. Strong oxidisers embrittle it. Anything above about 140°F deforms it. For all of those, stainless is the correct container, not a better grade of poly.
Do you buy empties back from a blending plant?
Yes, and chemical blending is our single largest source of inbound stock. If liquid arrives at your plant in totes and leaves in drums or pails, you are generating a stream of containers with real value. Standing collections on a weekly or monthly cycle are straightforward to set up.
How do I stop chloride attack on cages?
Keep brine and chloride products off the galvanising, which mostly means fixing drips and overfills rather than changing containers. Where chloride exposure is unavoidable — de-icer and road brine particularly — expect cage life to be shorter, inspect the lower members regularly, and consider stainless for the long-term asset.
Related pages
Industrial chemistry, coatings, oils and sanitation, in full
Specific gravity, wash programme, achievable grade, seal material and whether the container can ever be food-eligible again.
| Prior product | Family | SG | Programme | Best grade | Food? | Seal | What to watch |
|---|---|---|---|---|---|---|---|
| Sodium hydroxide 50% | Industrial chemistry | 1.52 | P1 | B | Never | EPDM | 3,497 lb filled — check every rating |
| Sodium hydroxide 25% | Industrial chemistry | 1.27 | P1 | B | Never | EPDM | Easy wash; dilute and drain |
| Potassium hydroxide 45% | Industrial chemistry | 1.46 | P1 | B | Never | EPDM | As NaOH; dense |
| Sulphuric acid 93% | Industrial chemistry | 1.83 | Refused | Dedicated | Never | PTFE | 4,182 lb filled; dedicated service only |
| Sulphuric acid 35% | Industrial chemistry | 1.26 | P1 | C | Never | PTFE | Fume attack on cage galvanising |
| Hydrochloric acid 31% | Industrial chemistry | 1.16 | P1 | C | Never | PTFE | Cage usually the limiting factor |
| Phosphoric acid 75% | Industrial chemistry | 1.58 | P1 | B | Never | PTFE | Dense; viscous at low temperature |
| Nitric acid 42% | Industrial chemistry | 1.26 | Refused | Dedicated | Never | PTFE | Oxidiser — embrittles HDPE |
| Hydrogen peroxide 35% | Industrial chemistry | 1.13 | P1 | B | Case by case | PTFE | Vent; absolutely no contaminants |
| Sodium hypochlorite 12% | Industrial chemistry | 1.21 | P1 | B | Never | EPDM | Degasses; vent and shield from UV |
| Ferric chloride 40% | Industrial chemistry | 1.42 | P2 | C | Never | Viton | Heavy orange staining is permanent |
| Aluminium sulphate | Industrial chemistry | 1.33 | P1 | B | Never | EPDM | Scale at the outlet boss |
| Polyaluminium chloride | Industrial chemistry | 1.35 | P1 | B | Never | EPDM | Gels if allowed to dry out |
| Propylene glycol coolant | Industrial chemistry | 1.04 | P1 | B | Never | EPDM | Ideal duty; nothing to watch |
| Ethylene glycol | Industrial chemistry | 1.11 | P1 | B | Never | EPDM | Toxic — never re-grade for potable |
| Calcium chloride brine 32% | Industrial chemistry | 1.38 | P1 | B | Never | Viton | Chloride attack on lower cage |
| Magnesium chloride de-icer | Industrial chemistry | 1.32 | P1 | B | Never | Viton | As above; rinse frames each spring |
| Potassium acetate de-icer | Industrial chemistry | 1.28 | P1 | B | Never | EPDM | Benign; airport runway chemistry |
| Urea solution (DEF) | Industrial chemistry | 1.09 | P1 | B | Never | EPDM | Purity-critical next fill; usually dedicated |
| Nickel plating solution | Industrial chemistry | 1.25 | Refused | Recycle | Never | Viton | Metal-bearing; never re-used |
| Phosphate conversion coating | Industrial chemistry | 1.22 | P2 | C | Never | Viton | Scale and staining |
| Amine corrosion inhibitor | Industrial chemistry | 0.98 | P2 | B | Never | Viton | Fish-like odour can persist |
| Sodium silicate | Industrial chemistry | 1.39 | P3 | C | Never | EPDM | Sets hard if dried; wash promptly |
| Polymer flocculant emulsion | Industrial chemistry | 1.02 | P3 | C | Never | EPDM | Extremely slippery; gels with water |
| Sodium bisulphite | Industrial chemistry | 1.33 | P1 | B | Never | EPDM | Sulphur odour; vent |
| Antifoam silicone emulsion | Industrial chemistry | 1.00 | P3 | C | Never | Viton | Film is very hard to remove |
| Latex paint, white | Coatings & inks | 1.30 | P3 | C | Never | EPDM | Heavy ghosting; often rebottle |
| Latex paint, tinted | Coatings & inks | 1.32 | P3 | C | Never | EPDM | Pigment ghosting permanent |
| Water-based pigment dispersion | Coatings & inks | 1.25 | P3 | C | Never | EPDM | Strong colour transfer into the wall |
| Flexographic ink | Coatings & inks | 1.08 | P3 | Rebottle | Never | Viton | Resin binder plasticises the surface |
| UV-curable coating | Coatings & inks | 1.10 | Refused | Recycle | Never | PTFE | Cures in the bottle; not washable |
| Acrylic adhesive emulsion | Coatings & inks | 1.08 | P3 | Rebottle | Never | EPDM | Caustic at 180°F, often still ghosts |
| PVA wood adhesive | Coatings & inks | 1.09 | P3 | C | Never | EPDM | Wash before it skins over |
| Polyurethane resin, 2-part | Coatings & inks | 1.12 | Refused | Recycle | Never | PTFE | Cross-linked; nothing shifts it |
| Asphalt emulsion | Coatings & inks | 1.01 | P3 | C | Never | Viton | Hot caustic plus long dwell |
| Concrete release agent | Coatings & inks | 0.89 | P2 | C | Never | Viton | Oily film; 140°F detergent |
| Mineral oil, hydraulic | Oils & fuels | 0.88 | P3 | B | Never | Viton | Permeation; faint odour often remains |
| Cutting fluid, soluble | Oils & fuels | 0.92 | P3 | B | Never | Viton | Bacterial odour is the real problem |
| Gear oil | Oils & fuels | 0.90 | P3 | C | Never | Viton | Heavy film; two cycles common |
| Diesel fuel | Oils & fuels | 0.85 | Refused | Recycle | Never | Viton | Permanent odour; bottle compromised |
| Kerosene | Oils & fuels | 0.81 | Refused | Recycle | Never | Viton | As diesel |
| Biodiesel B100 | Oils & fuels | 0.88 | P3 | C | Never | Viton | Solvency attacks some HDPE grades |
| Vegetable-based lubricant | Oils & fuels | 0.92 | P2 | B | Never | Viton | Oxidises to a varnish if left |
| Anionic surfactant concentrate | Cleaning & sanitation | 1.05 | P1 | B | Never | EPDM | It is soap — rinses, but foams |
| Non-ionic surfactant | Cleaning & sanitation | 1.03 | P1 | B | Never | EPDM | Easy wash |
| Alkaline degreaser | Cleaning & sanitation | 1.10 | P1 | B | Never | EPDM | Compatible with our own loop |
| Acid descaler | Cleaning & sanitation | 1.14 | P1 | B | Never | PTFE | Segregate heel from caustic tanks |
| Quaternary ammonium sanitiser | Cleaning & sanitation | 1.01 | P1 | B | Case by case | EPDM | Residual actives need verification |
| Peracetic acid sanitiser | Cleaning & sanitation | 1.12 | P1 | B | Case by case | PTFE | Oxidiser; vent and shield |
| Hand sanitiser (ethanol 70%) | Cleaning & sanitation | 0.87 | P1 | B | Case by case | Viton | Alcohol flashes off; little residue |
| Laundry detergent, liquid | Cleaning & sanitation | 1.06 | P1 | B | Never | EPDM | Optical brighteners can tint |
| Car wash soap concentrate | Cleaning & sanitation | 1.04 | P1 | B | Never | EPDM | Very common inbound stock |
| Floor finish / wax emulsion | Cleaning & sanitation | 1.02 | P3 | C | Never | EPDM | Films hard; wash before it dries |
| Prior product | SG | 275 gal filled | 330 gal filled | Seal | Programme |
|---|---|---|---|---|---|
| Sodium hydroxide 50% | 1.52 | 3,496 lb | 4,222 lb | EPDM | P1 |
| Sodium hydroxide 25% | 1.27 | 2,944 lb | 3,554 lb | EPDM | P1 |
| Potassium hydroxide 45% | 1.46 | 3,364 lb | 4,061 lb | EPDM | P1 |
| Sulphuric acid 93% | 1.83 | 4,181 lb | 5,049 lb | PTFE | Refused |
| Sulphuric acid 35% | 1.26 | 2,922 lb | 3,528 lb | PTFE | P1 |
| Hydrochloric acid 31% | 1.16 | 2,701 lb | 3,261 lb | PTFE | P1 |
| Phosphoric acid 75% | 1.58 | 3,629 lb | 4,382 lb | PTFE | P1 |
| Nitric acid 42% | 1.26 | 2,922 lb | 3,528 lb | PTFE | Refused |
| Hydrogen peroxide 35% | 1.13 | 2,634 lb | 3,181 lb | PTFE | P1 |
| Sodium hypochlorite 12% | 1.21 | 2,811 lb | 3,394 lb | EPDM | P1 |
| Ferric chloride 40% | 1.42 | 3,275 lb | 3,955 lb | Viton | P2 |
| Aluminium sulphate | 1.33 | 3,076 lb | 3,715 lb | EPDM | P1 |
| Polyaluminium chloride | 1.35 | 3,121 lb | 3,768 lb | EPDM | P1 |
| Propylene glycol coolant | 1.04 | 2,436 lb | 2,941 lb | EPDM | P1 |
| Ethylene glycol | 1.11 | 2,590 lb | 3,127 lb | EPDM | P1 |
| Calcium chloride brine 32% | 1.38 | 3,187 lb | 3,848 lb | Viton | P1 |
| Magnesium chloride de-icer | 1.32 | 3,054 lb | 3,688 lb | Viton | P1 |
| Potassium acetate de-icer | 1.28 | 2,966 lb | 3,581 lb | EPDM | P1 |
| Urea solution (DEF) | 1.09 | 2,546 lb | 3,074 lb | EPDM | P1 |
| Nickel plating solution | 1.25 | 2,900 lb | 3,501 lb | Viton | Refused |
| Phosphate conversion coating | 1.22 | 2,833 lb | 3,421 lb | Viton | P2 |
| Amine corrosion inhibitor | 0.98 | 2,303 lb | 2,780 lb | Viton | P2 |
| Sodium silicate | 1.39 | 3,209 lb | 3,875 lb | EPDM | P3 |
| Polymer flocculant emulsion | 1.02 | 2,391 lb | 2,887 lb | EPDM | P3 |
| Sodium bisulphite | 1.33 | 3,076 lb | 3,715 lb | EPDM | P1 |
| Antifoam silicone emulsion | 1.00 | 2,347 lb | 2,834 lb | Viton | P3 |
| Latex paint, white | 1.30 | 3,010 lb | 3,634 lb | EPDM | P3 |
| Latex paint, tinted | 1.32 | 3,054 lb | 3,688 lb | EPDM | P3 |
| Water-based pigment dispersion | 1.25 | 2,900 lb | 3,501 lb | EPDM | P3 |
| Flexographic ink | 1.08 | 2,524 lb | 3,047 lb | Viton | P3 |
| UV-curable coating | 1.10 | 2,568 lb | 3,101 lb | PTFE | Refused |
| Acrylic adhesive emulsion | 1.08 | 2,524 lb | 3,047 lb | EPDM | P3 |
| PVA wood adhesive | 1.09 | 2,546 lb | 3,074 lb | EPDM | P3 |
| Polyurethane resin, 2-part | 1.12 | 2,612 lb | 3,154 lb | PTFE | Refused |
| Asphalt emulsion | 1.01 | 2,369 lb | 2,860 lb | Viton | P3 |
| Concrete release agent | 0.89 | 2,104 lb | 2,540 lb | Viton | P2 |
| Mineral oil, hydraulic | 0.88 | 2,082 lb | 2,514 lb | Viton | P3 |
| Cutting fluid, soluble | 0.92 | 2,170 lb | 2,620 lb | Viton | P3 |
| Gear oil | 0.90 | 2,126 lb | 2,567 lb | Viton | P3 |
| Diesel fuel | 0.85 | 2,016 lb | 2,433 lb | Viton | Refused |
| Kerosene | 0.81 | 1,927 lb | 2,327 lb | Viton | Refused |
| Biodiesel B100 | 0.88 | 2,082 lb | 2,514 lb | Viton | P3 |
| Vegetable-based lubricant | 0.92 | 2,170 lb | 2,620 lb | Viton | P2 |
| Anionic surfactant concentrate | 1.05 | 2,458 lb | 2,967 lb | EPDM | P1 |
| Non-ionic surfactant | 1.03 | 2,413 lb | 2,914 lb | EPDM | P1 |
| Alkaline degreaser | 1.10 | 2,568 lb | 3,101 lb | EPDM | P1 |
| Acid descaler | 1.14 | 2,657 lb | 3,207 lb | PTFE | P1 |
| Quaternary ammonium sanitiser | 1.01 | 2,369 lb | 2,860 lb | EPDM | P1 |
| Peracetic acid sanitiser | 1.12 | 2,612 lb | 3,154 lb | PTFE | P1 |
| Hand sanitiser (ethanol 70%) | 0.87 | 2,060 lb | 2,487 lb | Viton | P1 |
| Laundry detergent, liquid | 1.06 | 2,480 lb | 2,994 lb | EPDM | P1 |
| Car wash soap concentrate | 1.04 | 2,436 lb | 2,941 lb | EPDM | P1 |
| Floor finish / wax emulsion | 1.02 | 2,391 lb | 2,887 lb | EPDM | P3 |
The four decisions after the product name
Format, grade, seal and weight — in that order, because each one constrains the next.
Container formats with full dimensional data
| Format | Nominal | Usable | L × W × H | Tare (steel base) | Gross, water | Outlet | Stack filled | Availability |
|---|---|---|---|---|---|---|---|---|
| 275 gal standard | 275 gal / 1,041 L | 265 gal | 48 × 40 × 46" | 137 lb | 2,347 lb | 2" S60x6 | 2 high | Ex-stock |
| 275 gal tall | 275 gal / 1,041 L | 264 gal | 48 × 40 × 53" | 141 lb | 2,342 lb | 2" S60x6 | 2 high | Regular |
| 330 gal standard | 330 gal / 1,249 L | 320 gal | 48 × 40 × 53" | 165 lb | 2,834 lb | 2" S60x6 | 2 high | Ex-stock |
| 350 gal | 350 gal / 1,325 L | 338 gal | 48 × 40 × 58" | 172 lb | 2,991 lb | 2" or 3" | 2 high | Occasional |
| 400 gal | 400 gal / 1,514 L | 386 gal | 48 × 46 × 60" | 198 lb | 3,417 lb | 3" buttress | 1 high | Order |
| 550 gal | 550 gal / 2,082 L | 532 gal | 48 × 48 × 72" | 251 lb | 4,688 lb | 3" buttress | 1 high | Occasional |
| 120 gal mini | 120 gal / 454 L | 115 gal | 32 × 32 × 36" | 71 lb | 1,030 lb | 2" S60x6 | 2 high | Occasional |
| 180 gal | 180 gal / 681 L | 174 gal | 40 × 40 × 42" | 98 lb | 1,549 lb | 2" S60x6 | 2 high | Order |
| Stainless 265 gal | 265 gal / 1,003 L | 258 gal | 48 × 40 × 50" | 285 lb | 2,436 lb | 2" tri-clamp | 2 high | Occasional |
| Stainless 330 gal | 330 gal / 1,249 L | 322 gal | 48 × 40 × 56" | 330 lb | 3,015 lb | 2" tri-clamp | 2 high | Occasional |
| Stainless 400 gal | 400 gal / 1,514 L | 390 gal | 48 × 46 × 62" | 385 lb | 3,637 lb | 3" tri-clamp | 1 high | Order |
| Stainless 500 gal | 500 gal / 1,893 L | 488 gal | 48 × 48 × 68" | 430 lb | 4,600 lb | 3" tri-clamp | 1 high | Order |
Grade matrix — what each condition commits us to
| Grade A | Grade B | Grade C | Cage / pallet only | |
|---|---|---|---|---|
| Bottle clarity | Clear / near-clear | Haze & staining permitted | Ghosting permitted | n/a |
| Prior service | Documented edible, signed at source | Industrial, declared | Industrial, declared | Any declared |
| Wash programme | Food line, recorded | Programme to residue, recorded | Ambient rinse | Cage rinse only |
| Hydrostatic test | 100% of units | Sampled | Sampled | n/a |
| New valve & gaskets | Yes, FDA-compliant | Yes | Sound or new | n/a |
| New lid | Yes | Yes | Sound or new | n/a |
| Re-marked | Yes | Yes | Where the plate survives | No |
| Stackable when filled | 2 high | 2 high | No | n/a |
| 30-day leak warranty | Yes | Yes | No — watertight at loading | No warranty |
| Food / potable | Yes, with records | No | No | n/a |
| Cost vs new | ≈ 35–45% | ≈ 25–32% | ≈ 18–24% | ≈ 5–10% |
| Lead time | Ex-stock to 5 days | Ex-stock | Ex-stock | Ex-stock |
| Loop score (lives left) | 5–6 | 4–5 | 2–3 | 3–4 bottles |
Seal compatibility — 21 media, four elastomers
| Medium | EPDM | Viton (FKM) | Silicone | PTFE | We would fit |
|---|---|---|---|---|---|
| Water, potable & process | Excellent | Excellent | Excellent | Excellent | EPDM |
| Dilute acids (<10%) | Good | Excellent | Fair | Excellent | EPDM |
| Concentrated acids | Poor | Good | Poor | Excellent | PTFE |
| Caustic soda, alkalis | Excellent | Fair | Fair | Excellent | EPDM |
| Liquid fertiliser, UAN | Excellent | Good | Fair | Excellent | EPDM |
| Glycols, coolants, de-icer | Excellent | Good | Good | Excellent | EPDM |
| Surfactants, detergents | Excellent | Good | Good | Excellent | EPDM |
| Edible oils, fats | Poor | Excellent | Poor | Excellent | Viton |
| Mineral oils | Poor | Excellent | Poor | Excellent | Viton |
| Aromatic solvents | Poor | Excellent | Poor | Excellent | Viton |
| Chlorinated solvents | Poor | Good | Poor | Excellent | Viton / PTFE |
| Ketones (acetone, MEK) | Fair | Poor | Poor | Excellent | PTFE |
| Alcohols | Good | Good | Good | Excellent | EPDM |
| Fuels, diesel, kerosene | Poor | Excellent | Poor | Excellent | Viton |
| Juice & syrup concentrate | Excellent | Excellent | Excellent | Excellent | FDA EPDM |
| Brine, pickling liquor | Good | Excellent | Fair | Excellent | Viton |
| Hot fill 140–180°F | Fair | Excellent | Excellent | Excellent | Viton / silicone |
| Hydrogen peroxide (dilute) | Good | Fair | Fair | Excellent | EPDM / PTFE |
| Sodium hypochlorite | Good | Good | Fair | Excellent | EPDM |
| Steam / CIP chemistry | Excellent | Fair | Good | Excellent | EPDM |
| Outdoor weathering & ozone | Excellent | Good | Excellent | Excellent | EPDM |
Filled weights and rack beam planning
| Product | SG | 275 gal filled | 330 gal filled | 550 gal filled |
|---|---|---|---|---|
| Acetone | 0.79 | 1,883 lb | 2,273 lb | 3,756 lb |
| Ethanol | 0.79 | 1,883 lb | 2,273 lb | 3,756 lb |
| Kerosene | 0.81 | 1,927 lb | 2,327 lb | 3,845 lb |
| Citrus terpene oil | 0.84 | 1,993 lb | 2,407 lb | 3,978 lb |
| Diesel fuel | 0.85 | 2,016 lb | 2,433 lb | 4,022 lb |
| Mineral oil, hydraulic | 0.88 | 2,082 lb | 2,514 lb | 4,155 lb |
| Biodiesel B100 | 0.88 | 2,082 lb | 2,514 lb | 4,155 lb |
| Concrete release agent | 0.89 | 2,104 lb | 2,540 lb | 4,200 lb |
| Gear oil | 0.90 | 2,126 lb | 2,567 lb | 4,244 lb |
| Canola oil | 0.91 | 2,148 lb | 2,594 lb | 4,289 lb |
| Soybean / olive oil | 0.92 | 2,170 lb | 2,620 lb | 4,333 lb |
| Flavour concentrate | 0.95 | 2,237 lb | 2,700 lb | 4,466 lb |
| Amine corrosion inhibitor | 0.98 | 2,303 lb | 2,780 lb | 4,599 lb |
| Water | 1.00 | 2,347 lb | 2,834 lb | 4,688 lb |
| Antifoam emulsion | 1.00 | 2,347 lb | 2,834 lb | 4,688 lb |
| Quaternary sanitiser | 1.01 | 2,369 lb | 2,860 lb | 4,732 lb |
| Asphalt emulsion | 1.01 | 2,369 lb | 2,860 lb | 4,732 lb |
| Maple sap | 1.02 | 2,391 lb | 2,887 lb | 4,777 lb |
| Non-ionic surfactant | 1.03 | 2,413 lb | 2,914 lb | 4,821 lb |
| Milk / dairy intermediate | 1.03 | 2,413 lb | 2,914 lb | 4,821 lb |
| Car wash soap concentrate | 1.04 | 2,436 lb | 2,941 lb | 4,865 lb |
| Propylene glycol | 1.04 | 2,436 lb | 2,941 lb | 4,865 lb |
| Anionic surfactant | 1.05 | 2,458 lb | 2,967 lb | 4,910 lb |
| Apple cider | 1.05 | 2,458 lb | 2,967 lb | 4,910 lb |
| Spent grain slurry | 1.05 | 2,458 lb | 2,967 lb | 4,910 lb |
| Laundry detergent | 1.06 | 2,480 lb | 2,994 lb | 4,954 lb |
| Flexographic ink | 1.08 | 2,524 lb | 3,047 lb | 5,043 lb |
| Wine / must | 1.08 | 2,524 lb | 3,047 lb | 5,043 lb |
| Acrylic adhesive emulsion | 1.08 | 2,524 lb | 3,047 lb | 5,043 lb |
| Urea solution (DEF) | 1.09 | 2,546 lb | 3,074 lb | 5,087 lb |
| Alkaline degreaser | 1.10 | 2,568 lb | 3,101 lb | 5,132 lb |
| Humic acid | 1.10 | 2,568 lb | 3,101 lb | 5,132 lb |
| Tomato paste | 1.10 | 2,568 lb | 3,101 lb | 5,132 lb |
| Ethylene glycol | 1.11 | 2,590 lb | 3,127 lb | 5,176 lb |
| Peracetic acid sanitiser | 1.12 | 2,612 lb | 3,154 lb | 5,220 lb |
| Fruit purée | 1.12 | 2,612 lb | 3,154 lb | 5,220 lb |
| Hydrogen peroxide 35% | 1.13 | 2,634 lb | 3,181 lb | 5,265 lb |
| Acid descaler | 1.14 | 2,657 lb | 3,207 lb | 5,309 lb |
| Hydrochloric acid 31% | 1.16 | 2,701 lb | 3,261 lb | 5,398 lb |
| Glyphosate concentrate | 1.17 | 2,723 lb | 3,287 lb | 5,442 lb |
| Brine 23% / soy sauce | 1.20 | 2,789 lb | 3,368 lb | 5,575 lb |
| Sodium hypochlorite 12% | 1.21 | 2,811 lb | 3,394 lb | 5,620 lb |
| Phosphate coating | 1.22 | 2,833 lb | 3,421 lb | 5,664 lb |
| Pigment dispersion | 1.25 | 2,900 lb | 3,501 lb | 5,797 lb |
| Nickel plating solution | 1.25 | 2,900 lb | 3,501 lb | 5,797 lb |
| Foliar micronutrient | 1.25 | 2,900 lb | 3,501 lb | 5,797 lb |
| Glycerine | 1.26 | 2,922 lb | 3,528 lb | 5,841 lb |
| Sulphuric acid 35% | 1.26 | 2,922 lb | 3,528 lb | 5,841 lb |
| Sodium hydroxide 25% | 1.27 | 2,944 lb | 3,554 lb | 5,886 lb |
| UAN 28 | 1.28 | 2,966 lb | 3,581 lb | 5,930 lb |
| Potassium acetate de-icer | 1.28 | 2,966 lb | 3,581 lb | 5,930 lb |
| Latex paint | 1.30 | 3,010 lb | 3,634 lb | 6,019 lb |
| UAN 32 fertiliser | 1.32 | 3,054 lb | 3,688 lb | 6,108 lb |
| Magnesium chloride de-icer | 1.32 | 3,054 lb | 3,688 lb | 6,108 lb |
| Liquid sugar / maple syrup | 1.33 | 3,076 lb | 3,715 lb | 6,152 lb |
| Ammonium thiosulphate | 1.33 | 3,076 lb | 3,715 lb | 6,152 lb |
| Aluminium sulphate | 1.33 | 3,076 lb | 3,715 lb | 6,152 lb |
| Juice concentrate (70 Bx) | 1.35 | 3,121 lb | 3,768 lb | 6,241 lb |
| Polyaluminium chloride | 1.35 | 3,121 lb | 3,768 lb | 6,241 lb |
| Liquid starter 10-34-0 | 1.38 | 3,187 lb | 3,848 lb | 6,374 lb |
| High-fructose corn syrup | 1.38 | 3,187 lb | 3,848 lb | 6,374 lb |
| Calcium chloride brine | 1.38 | 3,187 lb | 3,848 lb | 6,374 lb |
| Sodium silicate | 1.39 | 3,209 lb | 3,875 lb | 6,418 lb |
| Molasses / honey | 1.42 | 3,275 lb | 3,955 lb | 6,551 lb |
| Ferric chloride 40% | 1.42 | 3,275 lb | 3,955 lb | 6,551 lb |
| Calcium nitrate solution | 1.43 | 3,297 lb | 3,981 lb | 6,596 lb |
| Potassium hydroxide 45% | 1.46 | 3,364 lb | 4,061 lb | 6,729 lb |
| Potassium thiosulphate | 1.47 | 3,386 lb | 4,088 lb | 6,773 lb |
| Sodium hydroxide 50% | 1.52 | 3,496 lb | 4,222 lb | 6,995 lb |
| Phosphoric acid 75% | 1.58 | 3,629 lb | 4,382 lb | 7,261 lb |
| Sulphuric acid 93% | 1.83 | 4,181 lb | 5,049 lb | 8,370 lb |
| Configuration | Load per beam level | Rating needed |
|---|---|---|
| One 275 gal, water | 2,347 lb | 3,000 lb level |
| One 275 gal, SG 1.3 | 2,010 lb liquid + tare = 2,872 lb | 3,000 lb level, tight |
| Two 275 gal, water | 4,694 lb | 5,000 lb level |
| Two 275 gal, SG 1.3 | 5,744 lb | 6,000 lb level |
| Two 275 gal, SG 1.5 | 6,620 lb | 7,000 lb level |
| One 330 gal, water | 2,834 lb | 3,000 lb level, tight |
| Two 330 gal, water | 5,668 lb | 6,000 lb level |
| Two 330 gal, SG 1.3 | 6,936 lb | 7,000 lb level, tight |
| One 550 gal, water | 4,688 lb | 5,000 lb level |
| One 275 gal stainless, water | 2,436 lb | 3,000 lb level |
Wash programmes and turnaround
| Code | Programme | Temperature | Chemistry | Cycle | Relative cost | Suits |
|---|---|---|---|---|---|---|
| P1 | Ambient flood rinse | Ambient | Process water, occasional mild alkaline | 90 sec | 1.0× | Water-miscible residues |
| P2 | Hot detergent | 140°F | Alkaline detergent 1.5–2.5% | 3 min | 2.2× | Oils, fats, filming products |
| P3 | Caustic clean-in-place | 160–180°F | NaOH 2–4% + surfactant | 6–9 min | 4.5× | Pigments, latex, resins, heavy concentrates |
| PF | Food line (Bay 1) | 140°F | Alkaline detergent 2% + 100% hydrostatic | 3 min + test | 3.1× | Documented edible prior service |
| Refused | Not accepted | — | — | — | — | Unknown, acute, labelled-destruction, radiological |
Seasonality — when this sector is busiest
| Month | Food-grade demand | Industrial demand | Inbound supply | What it means for you |
|---|---|---|---|---|
| January | Low | High (de-icer) | Average | Winter emergencies; frozen heels slow the gate |
| February | High (maple starts) | High | Average | Sugaring floats go out; access often difficult |
| March | Highest (maple peak) | Moderate | Low | Freeze-damage crop arrives from last autumn |
| April | High | High (fertiliser) | Average | Maple returns, spring inputs ship |
| May | Average | Highest (fertiliser) | High | Biggest Grade B volume window |
| June | Average | High | High | Best month to sell us empties |
| July | Low | Average | Highest | Deepest stock; cheapest buying |
| August | Low | Average | Highest | Book autumn food-grade now |
| September | Highest (cider, crush) | High (de-icer fill) | Low | The squeeze begins |
| October | Highest | High | Lowest | Food-grade lead times stretch to 2–3 weeks |
| November | Average | Highest | Low | Winter chemistry fills; order covers and jackets |
| December | Average (juice runs) | High | Low | Holiday-week bookings close early |
Freight lanes and transit
| Destination | Distance | Transit | Mode | Equipment | Backhaul pricing |
|---|---|---|---|---|---|
| Harrisburg / Lancaster, PA | 35 mi | Same day | Flatbed / van | Own | Frequent |
| York / Hanover, PA | 12 mi | Same day | Flatbed | Own | Daily |
| Philadelphia, PA | 95 mi | Same day | Flatbed / van | Own | Daily |
| Allentown / Reading, PA | 80 mi | Same day | Flatbed | Own | Frequent |
| Pittsburgh, PA | 200 mi | Next day | Flatbed | Own | Twice weekly |
| Baltimore, MD | 60 mi | Same day | Flatbed / van | Own | Daily |
| Washington, DC | 95 mi | Same day | Van | Own | Frequent |
| Northern NJ / NYC | 175 mi | Next day | Van | Own | Frequent |
| Wilmington, DE | 75 mi | Same day | Flatbed | Own | Weekly |
| Richmond, VA | 230 mi | Next day | Flatbed | Own | Weekly |
| Norfolk, VA | 300 mi | 1–2 days | Flatbed | Own | Occasional |
| Buffalo / Rochester, NY | 300 mi | 1–2 days | Flatbed | Own | Weekly |
| Columbus, OH | 390 mi | 1–2 days | Flatbed | Own | Common |
| Cleveland, OH | 350 mi | 1–2 days | Flatbed | Own | Occasional |
| Charlotte, NC | 450 mi | 2 days | Flatbed | Partner | Occasional |
| Atlanta, GA | 700 mi | 2–3 days | Flatbed | Partner | Rare |
| Chicago, IL | 650 mi | 2 days | Flatbed | Partner | Occasional |
| Detroit, MI | 450 mi | 2 days | Flatbed | Partner | Occasional |
| Boston / New England | 400 mi | 2 days | Van | Partner | Occasional |
| Nashville, TN | 700 mi | 2–3 days | Flatbed | Partner | Rare |
| Dallas / Houston, TX | 1,450 mi | 3–4 days | Flatbed | Partner | Rare |
| Denver, CO | 1,700 mi | 4 days | Flatbed | Partner | No |
| Phoenix, AZ | 2,200 mi | 5 days | Flatbed | Partner | No |
| California | 2,700 mi | 5–6 days | Flatbed | Partner | No |
| Pacific Northwest | 2,700 mi | 5–6 days | Flatbed | Partner | No |
Standards and regulations
| Reference | Title | What it covers | Who it binds |
|---|---|---|---|
| 49 CFR 172.101 | Hazardous materials table | Classification and authorised packaging reference | Shippers |
| 49 CFR 172 Subpart H | Training | Who must be trained, in what, how often, with records | Any hazmat employer |
| 49 CFR 173 | Shippers — general requirements by class | Whether an IBC is authorised for your entry | Shippers |
| 49 CFR 178 Subpart N | IBC design types, testing and marking | What the plate means and how it was earned | Makers, reconditioners |
| 49 CFR 180.352 | Periodic inspection, testing, repair & remanufacture | 2.5-year visual, 5-year leakproofness + full inspection | Owners, shippers |
| 40 CFR 261.7 | RCRA empty containers | When a container counts as empty; P-list triple rinse | Generators |
| 40 CFR 262 | Generator standards | Waste determination, manifesting, accumulation | Generators |
| 21 CFR 177.1520 | Olefin polymers | HDPE compliance for food contact | Food users |
| 21 CFR 177.2600 | Rubber articles for repeated use | Gasket and seal compliance for food contact | Food users |
| 21 CFR 110 / 117 | Good manufacturing practice | Handling, storage, sanitation programmes | Food users |
| NSF/ANSI 61 | Drinking water system components | Potable-contact material evaluation | Water utilities |
| 29 CFR 1910.1200 | Hazard communication | Workplace labelling and safety data sheets | Everyone |
| 29 CFR 1910.146 | Permit-required confined spaces | Entry into tanks and vessels | Anyone cleaning containers |
| 29 CFR 1910.178 | Powered industrial trucks | Forklift operation and certification | Yards and docks |
| ANSI/ITSDF B56.1 | Low-lift and high-lift trucks | Capacity ratings and load centres | Yards and docks |
| ANSI MH16.1 | Steel storage racking | Beam capacity, deflection, inspection | Warehouses |
| PA Title 25 Ch. 95 | Wastewater treatment requirements | Industrial discharge standards in Pennsylvania | Wash lines |
| ISPM-15 | Wood packaging in international trade | Heat treatment and marking of timber pallets | Exporters |
Documents issued with every order
| Document | What it contains | When you get it |
|---|---|---|
| Written quotation | Unit price by grade, freight as its own line, validity, and the conditions that would change it | Before you order |
| Grade certificate | Assigned grade against our published definitions, per unit serial | With the order |
| Leak & pressure test record | Test pressure, hold time, outcome, per serial | With the order |
| Hydrostatic test certificate | 100% of food-line units, recorded against serial | Food-grade orders |
| Prior-contents declaration | Named last product, generating site, signature | Anything we collected |
| Wash programme record | Bay, programme, temperature, chemistry, cycle time | Reconditioned & contract work |
| Rinse verification | Final-rinse pH and conductivity | Reconditioned & contract work |
| Component specification | Valve, gasket, lid materials with compliance references | Food-grade orders |
| Photograph set | The actual units on the rack before loading | Every order |
| Weight ticket | Certified-scale gross weight and count | Collections and cleanouts |
| Diversion certificate | Unit counts, weights by stream, destination routes, dates | End-of-life batches |
| Certificate of insurance | GL, auto, cargo, workers' comp; additional insured | Before a crew arrives |
| Reconditioner marking detail | Code, date, design type | Re-marked units |
| Lease schedule | Count, grade, dates, weekly rate, return condition, replacement charge | Leases |
Why industrial buyers should default to Grade B
Every container in this photograph is watertight, leak tested and perfectly suited to fertiliser, surfactants, glycols, coolants, de-icer and the broad middle of chemical blending. The marks are prior-product staining, which is a price difference rather than a performance one.
The decisions that actually matter here are material of construction, elastomer selection, and marking status if a regulated liquid is going in. Bottle clarity is third at best, and buying Grade A for industrial service is the most common overspend in the sector.