Recycling is our
last service, not our first.
Granulating a container destroys the most valuable thing about it — its shape. So a bottle reaches our grinder only after failing reuse twice, and the cage and pallet are always assessed independently. Everything that does go is documented.
Quote documented end-of-life
Quantity, condition and whether you need a diversion certificate for reporting.
Tell us what you have.
We will tell you what it is worth.
Buying, selling, washing, hauling or recycling — one form covers all of it. Replies come from a specialist in York, PA, by email, inside one business day.
Prefer plain email? Write to info@ibctotesreco.com — include your ZIP, quantity and what the totes last held.
At true end of life an IBC separates into four streams: HDPE bottle → washed regrind, galvanised cage → steel recovery, pallet → steel, timber or composite recovery, and residue sludge → manifested disposal. Valves, lids and caps are harvested for reuse first. We issue a diversion certificate stating counts, weights, routes and dates.
The two-failure rule
A bottle does not reach the granulator because it is stained, old, or inconvenient. It reaches the granulator because it has failed twice: once at the inbound inspection bench, and again after a wash attempt where it still ghosted, still smelled, or still would not hold pressure. The cage and pallet are never judged by the bottle's failure — they are pulled, gauged and, if sound, fed straight into rebottling.
This sounds like a small procedural detail. It is actually the difference between a 97% diversion rate and a 60% one, because the overwhelming majority of “scrap totes” in this industry are scrapped whole when only one of their three components had failed.
Where the material actually goes
HDPE regrind. Bottles are cut, washed, granulated and screened. Post-industrial bulk-container HDPE is a clean, well-characterised feedstock, and it goes into non-food moulded and extruded products: drainage pipe, agricultural fittings, crates, pallets, composite lumber and geo-membrane components. It does not go back into food packaging, and anyone telling you otherwise about industrial-prior material should be asked how.
Galvanised steel. Cages and steel pallets go to a regional scrap partner. Steel is the single most reliably recycled material in the whole container, with no meaningful loss of properties across cycles.
Timber and composite pallets. Timber to chip and biomass recovery where it is clean; composite decks to plastics recovery.
Residue. Dewatered, characterised by prior-product class and consigned under manifest. This is the fraction that keeps us honest: it is the reason our published diversion figure is 97.4% rather than a round 100%.
Why we publish an awkward number
A yard claiming 100% diversion is either not counting residue sludge or not telling you about it. Ours is 97.4% by weight against certified scale tickets at the gate and at every outbound route, reconciled monthly. The method is set out on the Loop Ledger, including what we cannot measure well.
| Component | Weight | Route |
|---|---|---|
| HDPE bottle | ≈ 118 lb | Cut, washed, granulated |
| Galvanised cage | ≈ 62 lb | Steel scrap recovery |
| Steel pallet | ≈ 44 lb | Steel scrap recovery |
| Composite pallet | ≈ 31 lb | Plastics recovery |
| Timber pallet | ≈ 38 lb | Chip / biomass |
| Valve, lid, cap | ≈ 3 lb | Harvested or regrind |
| Residue heel & sludge | variable | Manifested disposal |
From your yard to a certificate
Five stages, each one leaving a weight ticket behind.
Declaration and assessment
You tell us the quantity, the last product and the condition. We quote: either we pay material value, or the lot is cost-neutral, or there is a handling charge. Nobody books a truck before that is in writing.
Collection and gate weight
Collected on our equipment or a partner lane, then across the certified scale at Emig Road. The gate weight is the denominator in everything that follows.
Last-chance reuse check
Even on a scrap lot, every unit passes the inspection bench. We routinely pull sound cages and the occasional perfectly reusable bottle out of lots that were sold to us as scrap, and we tell the seller when we do.
Separation and processing
Valves and lids harvested, bottle cut and granulated, cage and pallet separated to their streams, residue drained to the segregated tanks and dewatered.
Reconciliation and certificate
Outbound weights per stream reconciled against the gate weight. The diversion certificate states counts, weights by stream, destination routes and dates, and travels with the invoice.
Recycling FAQ
Can IBC totes be recycled?
Yes, completely, and in separate streams. The HDPE bottle is cut, washed and granulated into regrind that goes back into non-food moulded products. The galvanised cage is steel scrap with real value. The pallet goes to steel, timber or composite recovery depending on type. Valves and lids are harvested for reuse. Only residue sludge and a small contaminated fraction leave as waste — about 2.6% of our inbound weight.
Will you recycle totes that could still be reused?
No. A bottle reaches our granulator only after failing reuse twice: once at inbound grading and once after a wash attempt. We have no tonnage targets that would reward feeding sound containers into a grinder, and cages and pallets are always assessed independently of the bottle — which is the whole point of rebottling.
What is a diversion certificate?
A one-page document stating the unit count, weight by material stream, the destination route for each stream, and the date. It is built to drop straight into corporate waste or ESG reporting, and it is what auditors ask for when they want evidence rather than assurance. We issue one for every end-of-life batch on request.
Do you pay for scrap totes?
Usually yes, at material value rather than container value — the galvanised cage alone is worth something. Heavily contaminated lots, or lots where residue disposal costs exceed material recovery, can be cost-neutral or carry a handling charge. We will tell you which before anybody books a truck.
What happens to the residue?
Heels are drained to one of four segregated tanks by product family at the pre-drain station. Sludge from the settling and flotation stages is dewatered, characterised by prior-product class and consigned under manifest to a licensed facility. It is the least glamorous part of the operation and the part an auditor should ask about first.
Where does the HDPE regrind end up?
Non-food moulded and extruded products: drainage pipe, agricultural fittings, pallets, crates, geo-membrane components and composite lumber. Post-industrial HDPE from bulk containers is a clean, well-characterised feedstock, which is why it has a stable market even when mixed post-consumer plastics do not.
Related pages
Four streams, seven years of audited diversion
Weights, routes and the awkward 2.6% that cannot be diverted. Published because an unverified diversion claim is decoration.
| Year | Units in | Diversion | Manifested | Notable change |
|---|---|---|---|---|
| 2019 | 19,400 | 88.2% | 11.8% | Closed-loop water train commissioned |
| 2020 | 26,800 | 90.6% | 9.4% | Food line run six days a week |
| 2021 | 24,100 | 92.4% | 7.6% | Upcycled builds workshop opened |
| 2022 | 27,300 | 94.1% | 5.9% | Lease pool launched |
| 2023 | 29,600 | 96.1% | 3.9% | Diversion certificates formalised |
| 2024 | 31,200 | 96.8% | 3.2% | Stainless stream added |
| 2025 | 33,900 | 97.4% | 2.6% | Sludge dewatering upgraded |
| Component | Weight | Route | End market |
|---|---|---|---|
| HDPE bottle | ≈ 118 lb | Cut, washed, granulated | Drainage pipe, crates, composite lumber |
| Galvanised cage | ≈ 62 lb | Steel scrap recovery | Steel mills — no property loss |
| Steel pallet | ≈ 44 lb | Steel scrap recovery | Steel mills |
| Composite pallet | ≈ 31 lb | Plastics recovery | Moulded products |
| Timber pallet | ≈ 38 lb | Chip / biomass | Board, energy recovery |
| Valve, lid, cap | ≈ 3 lb | Harvested or regrind | Reuse first |
| Residue heel & sludge | Variable | Dewatered, manifested | Licensed facility |
How the numbers are produced
Diversion is a weight measurement and is therefore solid. Carbon is a calculation and we publish the inputs so you can disagree with it specifically.
Carbon by route — reuse, rebottle, recycle, repurpose
| Route | CO₂e | Fresh water | Virgin resin | Virgin steel |
|---|---|---|---|---|
| New unit | ≈ 410 lb | ≈ 290 gal | 118 lb | 62 lb |
| Rebottled | ≈ 182 lb | ≈ 120 gal | 47 lb | 0 lb |
| Reconditioned | ≈ 34 lb | ≈ 31 gal | 0 lb | 0 lb |
| Repurposed Grade C | ≈ 11 lb | ≈ 14 gal | 0 lb | 0 lb |
| Input | Quantity | Factor or source |
|---|---|---|
| Virgin HDPE resin | 118 lb / 53.5 kg | 1.8 kg CO₂e/kg |
| Blow moulding energy | 53.5 kg part | 0.4 kg CO₂e/kg |
| Hot-dip galvanised steel | 106 lb / 48 kg | 2.5 kg CO₂e/kg |
| Cage fabrication & assembly | 48 kg | 0.3 kg CO₂e/kg |
| Mechanical HDPE recycling | per kg processed | 0.5 kg CO₂e/kg |
| Fresh water per wash | 31 gal / unit | Metered |
| Natural gas, water heating | per programme | Metered per bay per shift |
| Electricity | per unit | Renewable tariff + 48 kW array |
| New valve, gaskets, lid | ≈ 3 lb | ≈ 8 lb CO₂e |
Prior products and what reaches end of life
| Prior product | Family | SG | Programme | Best grade | Food? | Seal | What to watch |
|---|---|---|---|---|---|---|---|
| Apple juice concentrate (70 Bx) | Food & beverage | 1.35 | PF | A | Yes | FDA EPDM | Best inbound stock we see; sugars rinse clean |
| Orange juice concentrate | Food & beverage | 1.33 | PF | A | Yes | FDA Viton | Citrus oil fraction can scent the bottle |
| Grape juice concentrate | Food & beverage | 1.34 | PF | A | Yes | FDA EPDM | Watch for tartrate scale at the outlet |
| Liquid sugar / sucrose syrup | Food & beverage | 1.33 | PF | A | Yes | FDA EPDM | Hot rinse only, no caustic needed |
| High-fructose corn syrup | Food & beverage | 1.38 | PF | A | Yes | FDA EPDM | Viscous; 3" outlet helps decanting |
| Molasses | Food & beverage | 1.42 | PF | A | Yes | FDA EPDM | Heated rinse; heavy heel |
| Honey | Food & beverage | 1.42 | PF | A | Yes | FDA EPDM | Crystallises; heater jacket recommended |
| Maple sap | Food & beverage | 1.02 | PF | A | Yes | FDA EPDM | Benign but sugars feed biofilm fast |
| Maple syrup | Food & beverage | 1.33 | PF | A | Yes | FDA EPDM | Hot rinse; inspect lid seat |
| Apple cider | Food & beverage | 1.05 | PF | A | Yes | FDA EPDM | Vented lid essential — ferments |
| Wine / must | Food & beverage | 1.08 | PF | A | Yes | FDA EPDM | Tartrate scale; usually leased |
| Beer / wort | Food & beverage | 1.05 | PF | A | Yes | FDA EPDM | Stainless preferred for repeat service |
| Brine (pickling liquor) | Food & beverage | 1.20 | PF | A | Yes | FDA Viton | Check cage for chloride attack |
| Vinegar, 10% | Food & beverage | 1.01 | PF | A | Yes | FDA EPDM | Easy; acid-resistant seal needed |
| Soy sauce | Food & beverage | 1.20 | PF | A | Yes | FDA Viton | Salt plus colour; monitor ghosting |
| Edible soybean oil | Food & beverage | 0.92 | P2 | A | Yes | FDA Viton | 140°F minimum or fat re-deposits |
| Edible canola oil | Food & beverage | 0.91 | P2 | A | Yes | FDA Viton | As above |
| Olive oil | Food & beverage | 0.92 | P2 | A | Yes | FDA Viton | Polyphenols can tint the wall |
| Glycerine, USP | Food & beverage | 1.26 | PF | A | Yes | FDA EPDM | Often effectively first-use stock |
| Propylene glycol, food grade | Food & beverage | 1.04 | PF | A | Yes | FDA EPDM | Frequently single-product filler stock |
| Liquid egg | Food & beverage | 1.04 | PF | A | Case by case | FDA EPDM | Protein film needs verification |
| Milk / dairy intermediate | Food & beverage | 1.03 | PF | A | Case by case | FDA EPDM | Allergen changeover record required |
| Whey concentrate | Food & beverage | 1.06 | PF | A | Case by case | FDA EPDM | Protein scale; hot detergent |
| Tomato paste | Food & beverage | 1.10 | PF | A | Yes | FDA Viton | Acidic; stains but rinses |
| Fruit purée | Food & beverage | 1.12 | PF | A | Yes | FDA EPDM | Pulp load; coarse settling matters |
| Flavour concentrate / essence | Food & beverage | 0.95 | Refused | Rebottle | No | PTFE | Permeates HDPE permanently — use stainless |
| Citrus terpene oil | Food & beverage | 0.84 | Refused | Recycle | Never | PTFE | One batch ends a poly bottle's usefulness |
| Spent grain slurry | Food & beverage | 1.05 | P2 | B | No | EPDM | By-product duty; 3" outlet strongly advised |
| Yeast slurry | Food & beverage | 1.08 | P2 | B | Case by case | EPDM | Vent — active fermentation |
| UAN 32 liquid nitrogen | Agricultural | 1.32 | P1 | B | Never | EPDM | Rinses readily; dense — check ratings |
| UAN 28 | Agricultural | 1.28 | P1 | B | Never | EPDM | As above |
| Liquid starter 10-34-0 | Agricultural | 1.38 | P1 | B | Never | EPDM | Polyphosphate scale at the outlet |
| Ammonium thiosulphate | Agricultural | 1.33 | P1 | B | Never | EPDM | Sulphur odour persists faintly |
| Potassium thiosulphate | Agricultural | 1.47 | P1 | B | Never | EPDM | Very dense; 275 format only |
| Calcium nitrate solution | Agricultural | 1.43 | P1 | B | Never | EPDM | Crystallises when cold |
| Humic / fulvic acid | Agricultural | 1.10 | P2 | B | Never | EPDM | Dark staining, usually washes out |
| Fish hydrolysate fertiliser | Agricultural | 1.12 | P3 | C | Never | Viton | Odour frequently permanent |
| Foliar micronutrient blend | Agricultural | 1.25 | P1 | B | Never | EPDM | Metal salts can tint the wall |
| Glyphosate concentrate | Agricultural | 1.17 | P3 | C | Never | Viton | Labelled rinse programme governs |
| 2,4-D amine concentrate | Agricultural | 1.19 | Refused | Per label | Never | Viton | Label prescribes rinse-and-destroy |
| Crop oil adjuvant | Agricultural | 0.88 | P3 | C | Never | Viton | Attacks EPDM; permeates slowly |
| Surfactant adjuvant (NIS) | Agricultural | 1.03 | P1 | B | Never | EPDM | Foams heavily on transfer |
| Molluscicide suspension | Agricultural | 1.22 | Refused | Per label | Never | Viton | Refused — labelled destruction |
| Livestock drinking water | Water & inert | 1.00 | P1 | A | Yes | EPDM | Effectively first-use |
| Irrigation water | Water & inert | 1.00 | P1 | A | Yes | EPDM | May carry silt; coarse settling |
| Sodium hydroxide 50% | Industrial chemistry | 1.52 | P1 | B | Never | EPDM | 3,497 lb filled — check every rating |
| Sodium hydroxide 25% | Industrial chemistry | 1.27 | P1 | B | Never | EPDM | Easy wash; dilute and drain |
| Potassium hydroxide 45% | Industrial chemistry | 1.46 | P1 | B | Never | EPDM | As NaOH; dense |
| Sulphuric acid 93% | Industrial chemistry | 1.83 | Refused | Dedicated | Never | PTFE | 4,182 lb filled; dedicated service only |
| Sulphuric acid 35% | Industrial chemistry | 1.26 | P1 | C | Never | PTFE | Fume attack on cage galvanising |
| Hydrochloric acid 31% | Industrial chemistry | 1.16 | P1 | C | Never | PTFE | Cage usually the limiting factor |
| Phosphoric acid 75% | Industrial chemistry | 1.58 | P1 | B | Never | PTFE | Dense; viscous at low temperature |
| Nitric acid 42% | Industrial chemistry | 1.26 | Refused | Dedicated | Never | PTFE | Oxidiser — embrittles HDPE |
| Hydrogen peroxide 35% | Industrial chemistry | 1.13 | P1 | B | Case by case | PTFE | Vent; absolutely no contaminants |
| Sodium hypochlorite 12% | Industrial chemistry | 1.21 | P1 | B | Never | EPDM | Degasses; vent and shield from UV |
| Ferric chloride 40% | Industrial chemistry | 1.42 | P2 | C | Never | Viton | Heavy orange staining is permanent |
| Aluminium sulphate | Industrial chemistry | 1.33 | P1 | B | Never | EPDM | Scale at the outlet boss |
| Polyaluminium chloride | Industrial chemistry | 1.35 | P1 | B | Never | EPDM | Gels if allowed to dry out |
| Propylene glycol coolant | Industrial chemistry | 1.04 | P1 | B | Never | EPDM | Ideal duty; nothing to watch |
| Ethylene glycol | Industrial chemistry | 1.11 | P1 | B | Never | EPDM | Toxic — never re-grade for potable |
| Calcium chloride brine 32% | Industrial chemistry | 1.38 | P1 | B | Never | Viton | Chloride attack on lower cage |
| Magnesium chloride de-icer | Industrial chemistry | 1.32 | P1 | B | Never | Viton | As above; rinse frames each spring |
| Potassium acetate de-icer | Industrial chemistry | 1.28 | P1 | B | Never | EPDM | Benign; airport runway chemistry |
| Urea solution (DEF) | Industrial chemistry | 1.09 | P1 | B | Never | EPDM | Purity-critical next fill; usually dedicated |
| Nickel plating solution | Industrial chemistry | 1.25 | Refused | Recycle | Never | Viton | Metal-bearing; never re-used |
| Chromic acid solution | Refused | 1.30 | Refused | Refused | Never | PTFE | Not accepted at the gate |
| Cyanide plating bath | Refused | 1.15 | Refused | Refused | Never | PTFE | Acutely hazardous — licensed facility only |
| Phosphate conversion coating | Industrial chemistry | 1.22 | P2 | C | Never | Viton | Scale and staining |
| Amine corrosion inhibitor | Industrial chemistry | 0.98 | P2 | B | Never | Viton | Fish-like odour can persist |
| Sodium silicate | Industrial chemistry | 1.39 | P3 | C | Never | EPDM | Sets hard if dried; wash promptly |
| Polymer flocculant emulsion | Industrial chemistry | 1.02 | P3 | C | Never | EPDM | Extremely slippery; gels with water |
| Sodium bisulphite | Industrial chemistry | 1.33 | P1 | B | Never | EPDM | Sulphur odour; vent |
| Antifoam silicone emulsion | Industrial chemistry | 1.00 | P3 | C | Never | Viton | Film is very hard to remove |
| Latex paint, white | Coatings & inks | 1.30 | P3 | C | Never | EPDM | Heavy ghosting; often rebottle |
| Latex paint, tinted | Coatings & inks | 1.32 | P3 | C | Never | EPDM | Pigment ghosting permanent |
| Water-based pigment dispersion | Coatings & inks | 1.25 | P3 | C | Never | EPDM | Strong colour transfer into the wall |
| Flexographic ink | Coatings & inks | 1.08 | P3 | Rebottle | Never | Viton | Resin binder plasticises the surface |
| UV-curable coating | Coatings & inks | 1.10 | Refused | Recycle | Never | PTFE | Cures in the bottle; not washable |
| Acrylic adhesive emulsion | Coatings & inks | 1.08 | P3 | Rebottle | Never | EPDM | Caustic at 180°F, often still ghosts |
| PVA wood adhesive | Coatings & inks | 1.09 | P3 | C | Never | EPDM | Wash before it skins over |
| Polyurethane resin, 2-part | Coatings & inks | 1.12 | Refused | Recycle | Never | PTFE | Cross-linked; nothing shifts it |
| Asphalt emulsion | Coatings & inks | 1.01 | P3 | C | Never | Viton | Hot caustic plus long dwell |
| Concrete release agent | Coatings & inks | 0.89 | P2 | C | Never | Viton | Oily film; 140°F detergent |
| Mineral oil, hydraulic | Oils & fuels | 0.88 | P3 | B | Never | Viton | Permeation; faint odour often remains |
| Cutting fluid, soluble | Oils & fuels | 0.92 | P3 | B | Never | Viton | Bacterial odour is the real problem |
| Gear oil | Oils & fuels | 0.90 | P3 | C | Never | Viton | Heavy film; two cycles common |
| Used motor oil | Refused | 0.89 | Refused | Recycle | Never | Viton | Waste stream — not accepted for reuse |
| Diesel fuel | Oils & fuels | 0.85 | Refused | Recycle | Never | Viton | Permanent odour; bottle compromised |
| Kerosene | Oils & fuels | 0.81 | Refused | Recycle | Never | Viton | As diesel |
| Biodiesel B100 | Oils & fuels | 0.88 | P3 | C | Never | Viton | Solvency attacks some HDPE grades |
| Vegetable-based lubricant | Oils & fuels | 0.92 | P2 | B | Never | Viton | Oxidises to a varnish if left |
| Anionic surfactant concentrate | Cleaning & sanitation | 1.05 | P1 | B | Never | EPDM | It is soap — rinses, but foams |
| Non-ionic surfactant | Cleaning & sanitation | 1.03 | P1 | B | Never | EPDM | Easy wash |
| Alkaline degreaser | Cleaning & sanitation | 1.10 | P1 | B | Never | EPDM | Compatible with our own loop |
| Acid descaler | Cleaning & sanitation | 1.14 | P1 | B | Never | PTFE | Segregate heel from caustic tanks |
| Quaternary ammonium sanitiser | Cleaning & sanitation | 1.01 | P1 | B | Case by case | EPDM | Residual actives need verification |
| Peracetic acid sanitiser | Cleaning & sanitation | 1.12 | P1 | B | Case by case | PTFE | Oxidiser; vent and shield |
| Hand sanitiser (ethanol 70%) | Cleaning & sanitation | 0.87 | P1 | B | Case by case | Viton | Alcohol flashes off; little residue |
| Laundry detergent, liquid | Cleaning & sanitation | 1.06 | P1 | B | Never | EPDM | Optical brighteners can tint |
| Car wash soap concentrate | Cleaning & sanitation | 1.04 | P1 | B | Never | EPDM | Very common inbound stock |
| Floor finish / wax emulsion | Cleaning & sanitation | 1.02 | P3 | C | Never | EPDM | Films hard; wash before it dries |
| Potable water | Water & inert | 1.00 | P1 | A | Yes | FDA EPDM | Frequently first-use stock |
| Deionised water | Water & inert | 1.00 | P1 | A | Yes | FDA EPDM | Best-value first-use source |
| Distilled water | Water & inert | 1.00 | P1 | A | Yes | FDA EPDM | As above |
| Glycerine, technical | Water & inert | 1.26 | P1 | B | No | EPDM | Technical grade is not food grade |
| Saline solution, industrial | Water & inert | 1.07 | P1 | B | Never | Viton | Chloride; inspect cage |
| Unknown or mixed residue | Refused | — | Refused | Refused | Never | — | Safety assessment, not a grading question |
| RCRA P-listed residue | Refused | — | Refused | Refused | Never | — | Licensed treatment facility only |
| Radiological material | Refused | — | Refused | Refused | Never | — | No testing, no discussion |
| Pesticide, labelled destruction | Refused | — | Refused | Refused | Never | — | Service life ended by regulation |
Failure modes — the two that send a unit to recycling
| Mode | Cause | What it looks like | Recoverable? | Prevention | Frequency |
|---|---|---|---|---|---|
| UV embrittlement | Unshaded outdoor storage | Chalky, boardy, higher-pitched tap | No | Cover or shade it | Most common |
| Stress whitening at the radius | Over-fill, freeze, uneven ground | White crackled lower corners | No | Level pad, respect max gross mass | Common |
| Plasticisation & ghosting | Pigment, resin, solvent absorption | Permanent shadow when backlit | Rebottle | Match chemistry to material | Common |
| Freeze damage | Left full and sealed | Bulged panel, split seam, blown boss | Sometimes fittings only | Drain or 2/3 fill, vented lid | Seasonal spike |
| Valve boss cracking | Unsupported pump or rigid pipe | Star crazing at the boss root | No — rebottle | Support the pump separately | Avoidable |
| Impact puncture | Forklift tine, drop, collision | Hole or deep gouge | No | Handling discipline | Rare |
| Cage racking | Soft ground, foot impact, over-fill | Diagonals differ by > 1/2" | Jig if under 1/2" | Level load-bearing pad | Common |
| Weld node cracking | Fatigue, previous field weld | Rust bloom then crack | No | Never field-weld a cage | Occasional |
| Pallet rot / delamination | Timber base outdoors | Soft bearers, split deck | Replace base | Specify steel or composite | Very common |
| Seal failure | Compression set, wrong elastomer, reuse | Weeping at the boss or lid | Yes — new seal | Replace at every product change | 71% of reports |
Regulations behind waste determination and manifesting
| Reference | Title | What it covers | Who it binds |
|---|---|---|---|
| 49 CFR 172.101 | Hazardous materials table | Classification and authorised packaging reference | Shippers |
| 49 CFR 172 Subpart H | Training | Who must be trained, in what, how often, with records | Any hazmat employer |
| 49 CFR 173 | Shippers — general requirements by class | Whether an IBC is authorised for your entry | Shippers |
| 49 CFR 178 Subpart N | IBC design types, testing and marking | What the plate means and how it was earned | Makers, reconditioners |
| 49 CFR 180.352 | Periodic inspection, testing, repair & remanufacture | 2.5-year visual, 5-year leakproofness + full inspection | Owners, shippers |
| 40 CFR 261.7 | RCRA empty containers | When a container counts as empty; P-list triple rinse | Generators |
| 40 CFR 262 | Generator standards | Waste determination, manifesting, accumulation | Generators |
| 21 CFR 177.1520 | Olefin polymers | HDPE compliance for food contact | Food users |
| 21 CFR 177.2600 | Rubber articles for repeated use | Gasket and seal compliance for food contact | Food users |
| 21 CFR 110 / 117 | Good manufacturing practice | Handling, storage, sanitation programmes | Food users |
| NSF/ANSI 61 | Drinking water system components | Potable-contact material evaluation | Water utilities |
| 29 CFR 1910.1200 | Hazard communication | Workplace labelling and safety data sheets | Everyone |
| 29 CFR 1910.146 | Permit-required confined spaces | Entry into tanks and vessels | Anyone cleaning containers |
| 29 CFR 1910.178 | Powered industrial trucks | Forklift operation and certification | Yards and docks |
| ANSI/ITSDF B56.1 | Low-lift and high-lift trucks | Capacity ratings and load centres | Yards and docks |
| ANSI MH16.1 | Steel storage racking | Beam capacity, deflection, inspection | Warehouses |
| PA Title 25 Ch. 95 | Wastewater treatment requirements | Industrial discharge standards in Pennsylvania | Wash lines |
| ISPM-15 | Wood packaging in international trade | Heat treatment and marking of timber pallets | Exporters |
Documents issued on an end-of-life batch
| Document | What it contains | When you get it |
|---|---|---|
| Written quotation | Unit price by grade, freight as its own line, validity, and the conditions that would change it | Before you order |
| Grade certificate | Assigned grade against our published definitions, per unit serial | With the order |
| Leak & pressure test record | Test pressure, hold time, outcome, per serial | With the order |
| Hydrostatic test certificate | 100% of food-line units, recorded against serial | Food-grade orders |
| Prior-contents declaration | Named last product, generating site, signature | Anything we collected |
| Wash programme record | Bay, programme, temperature, chemistry, cycle time | Reconditioned & contract work |
| Rinse verification | Final-rinse pH and conductivity | Reconditioned & contract work |
| Component specification | Valve, gasket, lid materials with compliance references | Food-grade orders |
| Photograph set | The actual units on the rack before loading | Every order |
| Weight ticket | Certified-scale gross weight and count | Collections and cleanouts |
| Diversion certificate | Unit counts, weights by stream, destination routes, dates | End-of-life batches |
| Certificate of insurance | GL, auto, cargo, workers' comp; additional insured | Before a crew arrives |
| Reconditioner marking detail | Code, date, design type | Re-marked units |
| Lease schedule | Count, grade, dates, weekly rate, return condition, replacement charge | Leases |
- Declaration and assessment. Quantity, last product, condition. We quote: material value, cost-neutral, or a handling charge — in writing, before a truck is booked.
- Collection and gate weight across a certified scale. That weight is the denominator in everything that follows.
- Last-chance reuse check. Even on a scrap lot, every unit passes the bench. We routinely pull sound cages out of lots sold to us as scrap, and we say so.
- Separation and processing. Valves and lids harvested, bottle cut and granulated, cage and pallet to their streams, residue drained and dewatered.
- Reconciliation and certificate. Outbound weights per stream against the gate weight; the certificate states counts, weights, routes and dates.
Four ways diversion figures get inflated — ask us these too
Counting units instead of weight
Ninety-nine containers diverted and two tonnes of sludge manifested is 99% by count and perhaps 80% by weight. Sludge does not come in units.
Shrinking the denominator
Measuring against “waste arising” rather than inbound gate weight. Ask what weight the percentage is a percentage of.
Scoring recycling as equal to reuse
A reconditioned tote is ≈ 34 lb CO₂e; the new unit it displaced is ≈ 410 lb. Diversion is a binary and a poor ceiling.
Omitting residue
Every wash line produces sludge. A reconditioner who cannot describe how theirs is characterised and consigned is either washing little or not saying something.
Even on a scrap lot, every unit crosses the bench
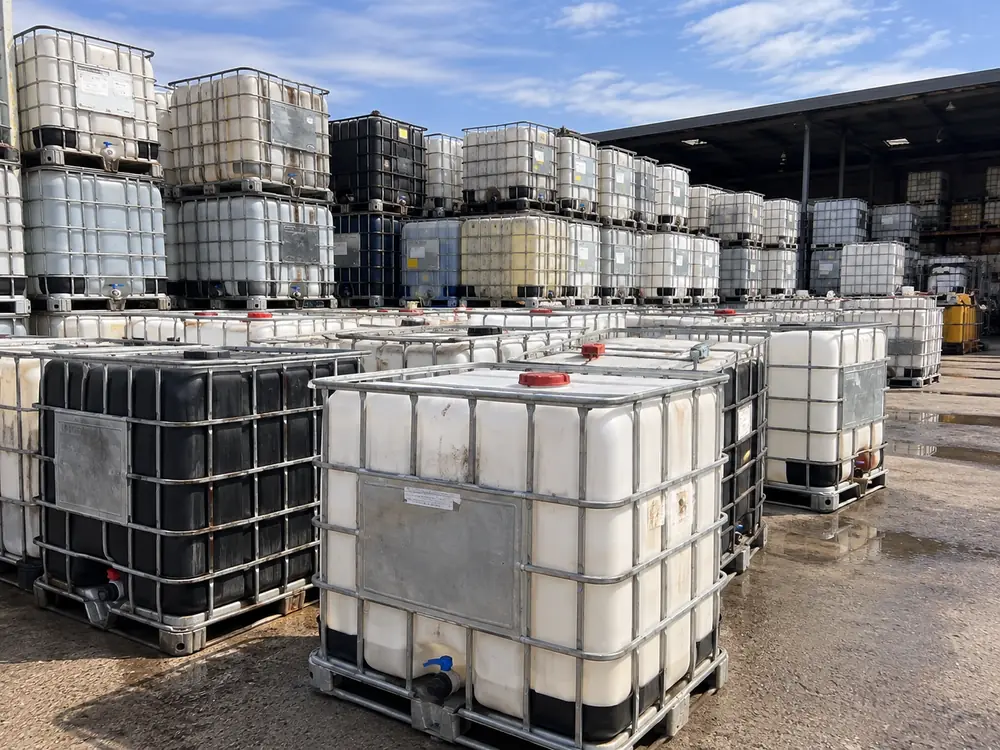
The containers in this photograph were sold to us as scrap. Several of them were not: a bottle that backlit clean, four cages that measured square within a quarter of an inch, a dozen valves worth harvesting.
That last-chance check is the third stage of every end-of-life batch, and it is the reason our diversion figure has a decimal point in it rather than a round number. What genuinely cannot be reused separates into HDPE regrind, steel, timber or composite recovery, and a manifested residue stream.